Product safety is one of the highest priorities in the pharmaceutical industry because medications and healthcare products must remain secure throughout storage, transportation, and distribution. Reliable packaging helps protect sensitive products from damage while maintaining organization and reducing handling risks. Well designed interior packaging also supports efficient logistics and enhances product integrity across the supply chain.
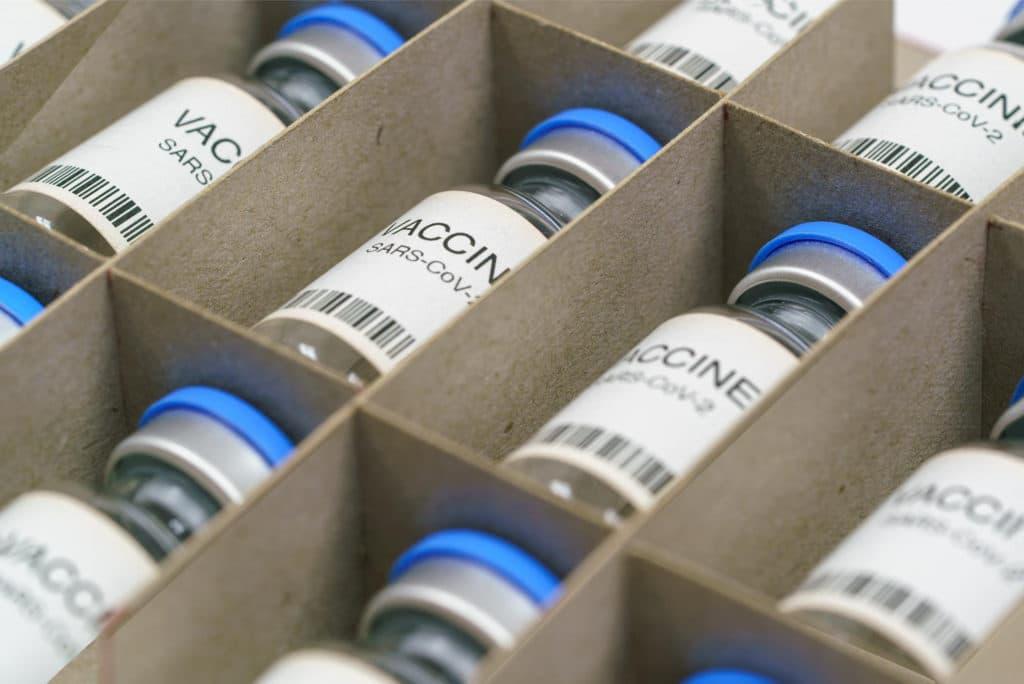
Pharmaceutical packaging box partitions provide an effective solution for separating medical products inside cartons, preventing movement, and minimizing the risk of damage during shipping. These customized partitions create individual compartments that improve stability, protect fragile containers, and support consistent packaging quality. As pharmaceutical distribution continues to expand, dependable partition solutions remain essential for maintaining product safety and operational efficiency.
Understanding Pharmaceutical Packaging Box Partitions
What Are Pharmaceutical Packaging Box Partitions
Pharmaceutical packaging box partitions are interior dividers specifically designed to organize and protect medical products inside shipping cartons. These partitions create individual compartments that securely hold bottles, vials, ampoules, syringes, and other healthcare products. Proper compartmentalization prevents products from coming into direct contact during transportation. Well designed partitions improve product stability while supporting efficient packaging operations.
Why They Are Essential in Pharmaceutical Packaging
Pharmaceutical products require greater protection than many other packaged goods because they are often fragile, sensitive, and high in value. Damaged packaging may affect product quality and increase replacement costs. Interior partitions help reduce these risks by stabilizing products throughout shipping and storage. Reliable packaging supports safe handling from manufacturing facilities to healthcare providers and pharmacies.
Benefits of Pharmaceutical Packaging Box Partitions
Enhanced Product Protection
One of the most significant benefits of pharmaceutical packaging box partitions is their ability to reduce product damage. Individual compartments prevent containers from colliding with each other during transportation. This separation minimizes the possibility of cracks, scratches, broken seals, and damaged labels. Better protection helps maintain product quality and customer confidence.
Improved Packaging Organization
Organized packaging simplifies handling, storage, and inventory management throughout the supply chain. Clearly separated products are easier to inspect, count, and distribute. Consistent product placement also improves packing accuracy and reduces handling errors during production. Efficient organization contributes to smoother operational workflows.
Increased Shipping Reliability
Medical products often travel long distances through multiple distribution centers before reaching their destinations. Secure partitions help maintain product stability despite vibration, stacking pressure, and repeated handling. Reliable packaging reduces shipping related damage while improving overall distribution performance. Businesses benefit from fewer product losses and improved customer satisfaction.
How Pharmaceutical Packaging Box Partitions Improve Product Safety
Preventing Product Movement
Movement inside shipping cartons is one of the leading causes of packaging damage. Pharmaceutical packaging box partitions create secure compartments that hold each product firmly in place throughout transportation. Stable positioning reduces impact between containers and helps preserve product integrity. Proper separation also protects packaging labels and closures from unnecessary wear.
Reducing Breakage
Glass vials, medicine bottles, and laboratory containers require dependable interior protection. Well designed partitions create protective barriers that absorb movement and reduce direct impact between products. This additional support lowers the likelihood of breakage during loading, transportation, and warehouse storage. Fewer damaged products improve operational efficiency and reduce replacement costs.
Supporting Safe Storage
Medical products are frequently stored in warehouses before shipment to healthcare facilities and pharmacies. Interior partitions help maintain product organization while preventing containers from shifting inside stacked cartons. Stable packaging supports safe storage conditions and simplifies inventory management throughout distribution operations.
Materials Used for Pharmaceutical Packaging Box Partitions
Corrugated Material
Corrugated material offers excellent strength and impact resistance for pharmaceutical packaging applications. Its layered construction helps absorb transportation shocks while maintaining carton stability. Corrugated partitions are suitable for products requiring additional structural support during long distance shipping.
Chipboard Material
Chipboard partitions provide a lightweight and economical solution for many pharmaceutical packaging applications. Their smooth finish and consistent construction create organized compartments that maintain reliable product separation. Chipboard supports efficient packaging while improving product presentation.
SBS Material
Solid bleached sulfate material combines durability with a clean and professional appearance. Its smooth surface makes it suitable for premium pharmaceutical packaging where both protection and presentation are important. SBS partitions provide dependable compartment separation while enhancing overall package quality.
Pharmaceutical Products That Benefit from Box Partitions
Medicine Bottles
Prescription and over the counter medicine bottles require secure packaging to prevent collisions during transportation. Interior partitions create individual spaces that protect bottles from impact while maintaining organized packaging. Reliable separation helps preserve product quality throughout distribution.
Glass Vials
Glass vials are among the most delicate pharmaceutical packaging components. Customized partitions reduce movement and provide dependable protection against vibration and accidental impacts. Stable packaging significantly lowers the risk of breakage during shipping.
Laboratory Products
Diagnostic kits, laboratory samples, and medical testing products require careful handling throughout transportation. Partitioned packaging helps organize these items while minimizing movement inside cartons. Improved organization also simplifies receiving and inventory procedures.
Medical Devices
Many medical devices include sensitive components that require additional protection during shipping. Interior partitions help stabilize these products while preventing contact with other packaged items. Secure packaging reduces cosmetic damage and supports safe delivery.
Factors to Consider When Choosing Pharmaceutical Packaging Box Partitions
Product Dimensions
Accurate measurements ensure partitions provide a secure fit for every product. Proper compartment sizing minimizes movement while maximizing available packaging space. Well fitted partitions improve both product protection and packing efficiency.
Product Weight
The weight of pharmaceutical products influences partition material selection and structural design. Heavier products often require stronger materials to maintain stability throughout transportation. Matching partition strength to product weight improves long term packaging performance.
Shipping Conditions
Distribution methods expose pharmaceutical products to vibration, stacking pressure, and repeated handling. Packaging should be designed according to actual transportation conditions to provide dependable protection. Appropriate partition selection reduces shipping related damage.
Regulatory Expectations
Pharmaceutical packaging should support careful handling and consistent product organization throughout the supply chain. Reliable partition systems contribute to packaging quality while helping businesses maintain high operational standards. Well engineered packaging also supports efficient quality control procedures.
Best Practices for Using Pharmaceutical Packaging Box Partitions
Perform Packaging Testing
Packaging should be tested under realistic transportation conditions before large production runs begin. Testing confirms that partitions provide adequate protection against impact and vibration. Early evaluation helps identify improvements before products enter distribution.
Maintain Quality Inspections
Routine inspection of partition materials and finished packaging helps maintain consistent product protection. Quality monitoring reduces packaging variation while supporting reliable pharmaceutical distribution. Consistent inspection contributes to improved operational performance.
Update Packaging Designs
Pharmaceutical products and packaging requirements may change over time. Regular reviews ensure partition designs continue meeting current product specifications and transportation needs. Continuous improvement supports long term packaging effectiveness.
Future Trends in Pharmaceutical Packaging Partitions
Advancements in packaging technology continue improving product protection, manufacturing precision, and operational efficiency. Modern engineering methods allow customized partition designs that provide greater accuracy while supporting faster production. Businesses increasingly invest in packaging systems that balance dependable protection with efficient material utilization. As pharmaceutical distribution continues expanding worldwide, customized box partitions will remain a vital component of safe and reliable packaging.
Conclusion
Pharmaceutical packaging box partitions play a critical role in protecting sensitive healthcare products throughout storage, handling, and transportation. Carefully designed partitions reduce product movement, minimize breakage, improve organization, and support efficient packaging operations across the pharmaceutical supply chain. Investing in dependable interior packaging helps businesses maintain product quality while improving customer confidence and operational reliability. General Partition Co Inc provides expertly manufactured packaging partition solutions designed to support pharmaceutical companies with customized interior packaging, dependable product protection, and efficient packaging systems that meet the demanding requirements of modern healthcare distribution.



 English
 Arabic
 French
 Spanish
 Portuguese
 Deutsch
 Dutch
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)
 Greek